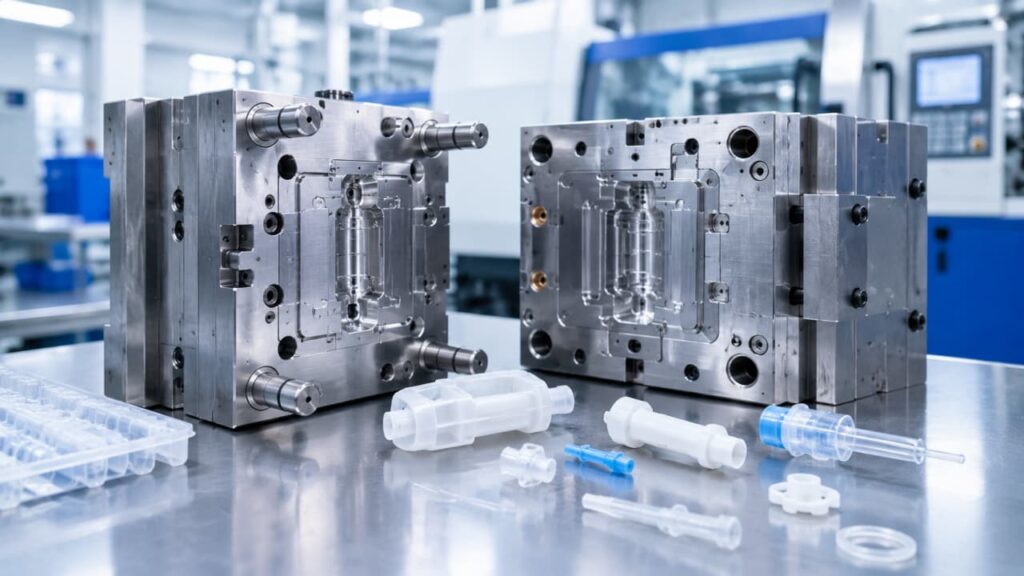
Medical device injection molding produces sterile, tight-tolerance plastic components for healthcare applications by injecting medical-grade resin into a precision mold. It is the right choice when you need thousands of identical parts per year and the resin can survive your sterilization method. For low volumes, parts still in design flux, or components that must be machined from metal, CNC machining is usually cheaper. Material selection is governed by three gates: confirm the resin is actually medical-grade, match it to your sterilization method, and verify biocompatibility for the specific contact type.
What Is Medical Device Injection Molding?
Medical device injection molding is the same core process used for consumer plastics — melt resin, inject it into a steel mold, cool, eject — but wrapped in a quality system built for healthcare. The part geometry is identical part to part only because the process, not the operator, makes it.
How It Differs From Standard Injection Molding
- Validation: production runs follow IQ/OQ/PQ (installation, operational, performance qualification) so the process is documented as repeatable.
- Traceability: resin lot, machine, tool, and inspection records link every finished part back to its raw material.
- Documentation: material certifications and change control are part of the deliverable, not an afterthought.
The Six-Step Process
- Material selection and drying — the medical-grade resin is dried to a controlled moisture level; residual moisture causes splay and weak welds.
- Mold design and tooling — gate, runner, cooling, and venting are set at the mold fabrication stage; they cannot be changed cheaply later.
- Injection and cavity fill — dimensional accuracy is established here.
- Cooling and solidification — typically the longest part of the cycle; uniform cooling prevents warpage and sink marks.
- Ejection and trimming — gates and flash are removed; critical parts are handled to avoid contamination.
- Quality control and validation — dimensional and visual inspection against the validated process window.
A DFM (design-for-manufacturability) review before steel is cut prevents most of the defects above.
Should You Use Injection Molding or CNC Machining?
This is the first question to answer, and the one most vendor guides skip. Injection molding is not automatically cheaper — its per-part cost advantage only appears once you spread the mold cost across enough units.
The Volume Crossover
Injection molding needs a mold, which is a fixed investment that can range from a few thousand dollars for a simple single-cavity tool to substantially more for multi-cavity or complex molds. CNC machining needs no mold. As a general industry rule of thumb, molding starts to beat machining on per-part cost somewhere in the low thousands of units per year; below that, machining is usually the cheaper path. The exact crossover depends on part complexity, tooling cost, and resin — see our notes on low vs high volume molding and the factors that drive molding cost.
| Factor | Injection Molding | CNC Machining |
|---|---|---|
| Upfront tooling | Required (fixed cost) | None (fixtures only) |
| Best volume | Thousands+ per year | Prototypes to low volume |
| Design change cost | High (modify or rebuild mold) | Low (update program) |
| Lead time to first parts | Longer (mold build) | Shorter |
| Part-to-part consistency | Excellent at volume | Excellent |
When Injection Molding Is the Wrong Choice
- Annual volume stays in the hundreds, not thousands.
- The design is still changing — every revision risks scrapping mold steel.
- The part must be machined from metal for strength or radiopacity.
- You need a handful of functional test units this week, not a production run.
A Hybrid Path: Prototype, Validate, Then Tool Up
Most medical programs do not jump straight to a mold. Teams prove form, fit, and function with rapid prototyping — 3D printing for form, CNC machining for functional parts, and vacuum casting for small bridge runs — then commit to tooling once the design is locked. This compresses timeline and protects the mold investment.
Common Medical Injection Molding Processes
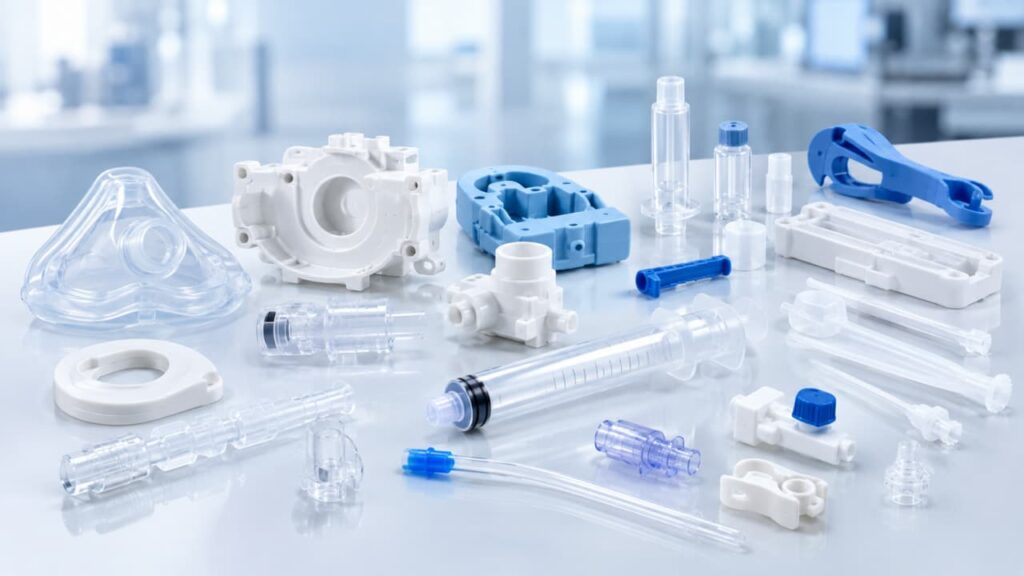
The “medical injection molding” label covers several distinct processes. Pick by the part, not by habit.
Thin-Wall Molding
Used for disposable consumables (syringe barrels, pipette tips, petri dishes) where wall sections fall below roughly 1 mm. It cuts material and cycle time but demands tight process control to fill thin sections without short shots.
Insert Molding
Encapsulates a pre-formed component — a metal pin, a ceramic sensor, or an already-molded plastic part — in resin during the molding cycle. If the core is metal, ceramic, or any non-molded preform, you need insert molding, not overmolding. For the distinction, see insert molding vs overmolding. A common failure is relying on resin shrinkage alone to hold a dissimilar insert: for metal or ceramic cores, add mechanical retention (knurls, flares, or a textured surface) or the seal leaks.
Overmolding and Two-Shot Molding
Overmolding bonds a second material — usually a soft TPE or TPU — onto an already-molded rigid substrate to make grips, seals, and dampers. Overmolding applications span surgical handles, drug-delivery devices, and enclosures. Two-shot molding produces the same result in one machine cycle and is preferred at higher volumes; material compatibility is the deciding factor, covered in our TPE/TPU overmolding materials guide.
Liquid Silicone Rubber (LSR) Molding
LSR is a flexible, inherently biocompatible elastomer molded in a heated, two-part process. It tolerates all common sterilization methods and is used for seals, valves, and soft components where a thermoplastic cannot flex enough.
Choosing Medical-Grade Materials
This is where medical programs fail most often — not because the resin is weak, but because the selection ignored sterilization or biocompatibility.
Gate 1 — Confirm the Resin Is Actually Medical-Grade
“PP” is a chemical family, not a qualification. A medical-grade resin is a specific grade with a documented change-control history and a data package showing USP Class VI and/or ISO 10993 biocompatibility. Always ask the supplier for the grade name and the supporting certificates, not just the polymer type. See our medical injection molding materials guide and the engineering-plastic selection method.
Gate 2 — Match the Resin to Your Sterilization Method
Sterilization stresses the polymer. A resin that is fine for EtO may craze or yellow under autoclave steam. Choose the resin after you know the sterilization method, not before.
| Resin | Autoclave (steam) | Gamma radiation | Ethylene oxide (EtO) | Typical medical use |
|---|---|---|---|---|
| Polypropylene (PP) | Compatible | Compatible | Compatible | Disposable consumables, syringes |
| Polyethylene (PE, UHMW) | Compatible | Compatible | Compatible | Catheters, orthopaedic bearings |
| Polycarbonate (PC) | Risk of hydrolysis/yellowing in many grades | Compatible | Compatible | Housings, connectors, fluidic parts |
| PEI (Ultem) | Stable (high cycle count) | Compatible | Compatible | Reusable instruments |
| PEEK | Stable | Stable | Compatible | High-performance, implant-adjacent parts |
| PPSU | Stable (high cycle count) | Compatible | Compatible | Reusable instruments, trays |
| LSR (silicone) | Compatible | Compatible | Compatible | Seals, valves, soft components |
Compatibility depends on the specific grade and sterilization cycle parameters. Confirm against the resin supplier’s documented data before tooling is cut — this cannot be corrected after the mold is built.
Gate 3 — Verify Biocompatibility for the Contact Type
Biocompatibility is not a property of the resin alone. It is the result of resin + additives + colorants + sterilization method + contact type and duration. A material safe for brief surface contact may not be acceptable for long-term implantation. Evaluate it against ISO 10993 for your specific device, not the material family.
Resin Quick-Reference
- PP / PE — low cost, broad sterilization tolerance; the default for disposables.
- PC — clarity and impact strength; watch autoclave exposure.
- PEI / PPSU / PEEK — high heat and sterilization stability; chosen for reusable instruments.
- LSR — flexible, biocompatible, all-method sterilization.
Regulatory and Quality Considerations
Device Classification Drives Evidence Depth
Regulatory load scales with risk. Non-invasive, low-risk devices (roughly Class I) need lighter evidence than implantable or life-supporting devices (Class III). The exact pathway — and whether you file under FDA 510(k), PMA, or EU MDR — depends on intended use and market; that is the device maker’s responsibility, not the molder’s. What the molder must provide is the manufacturing evidence underneath it.
ISO 13485 and Process Validation
ISO 13485 is the quality-management baseline for medical device manufacturing. Under it, molding programs run IQ/OQ/PQ and keep lot-level traceability. GoodTech holds ISO 13485 certification for medical devices; details are on our quality system page and in our ISO 13485 medical molding guide.
What Your Supplier Must Document
- Material certificates (grade, lot, biocompatibility data)
- Machine and tool identification per lot
- IQ/OQ/PQ validation records
- Inspection results against the drawing
- Change-control records for any material or process change
Use our supplier audit checklist when you qualify a molder.
Design and Quality Checklist
- Run a DFM review before the mold is cut.
- Keep wall thickness uniform to avoid sink and warp.
- Specify tight tolerances only on critical-to-quality features — see the tolerances guide.
- Plan gate location and venting for the sterilization method.
- Prevent common defects early with the defect prevention guide.
How to Choose a Medical Injection Molding Supplier
Price is the last thing to compare. Evaluate first:
- Certifications — ISO 13485 for medical; ask for the scope.
- Engineering support — can they run a DFM review and catch issues before tooling?
- Material documentation — can they source and certify the grade you need?
- Traceability and validation — IQ/OQ/PQ, lot records, change control.
- Communication and IP — clear drawing handling and IP protection when sourcing from China; see our working-with-a-China-supplier guide.
Common Mistakes in Medical Injection Molding
- Choosing the resin before locking the sterilization method.
- Assuming “biocompatible” is a property of the plastic family.
- Ignoring volume economics and tooling up for a part that will never hit volume.
- Relying on resin shrinkage alone to hold a dissimilar insert — add mechanical retention.
- Treating documentation as optional until the auditor arrives.
Why GoodTech for Medical Device Injection Molding
GoodTech is an ISO 13485-certified molding partner serving the medical device industry alongside consumer electronics and food equipment. Our capabilities cover plastic injection molding — including insert molding, overmolding, and two-shot molding — for parts from 0.2 g to 4,500 g, on 45 molding machines rated 60 to 1,000 tons. U.S.-based engineers in Chicago support quotes and DFM reviews, while our Shenzhen team manages production and our Vietnam site supports tariff-sensitive programs.
To get an accurate quote, send us your 3D model, expected annual volume, target material or sterilization method, device class and contact type, and any critical tolerances. We will return a DFM review and a molded-part cost based on your real numbers — not a generic estimate. Request a quote and DFM review.
Key Takeaways
- Injection molding wins on per-part cost only above a few-thousand-units/yr threshold; otherwise machine.
- Pick the process by the part: thin-wall, insert, overmolding/two-shot, or LSR.
- Material selection has three gates: medical-grade confirmation, sterilization compatibility, biocompatibility for the contact type.
- Biocompatibility is a combination result, not a resin property.
- Require ISO 13485, IQ/OQ/PQ, and lot-level traceability from your supplier.
FAQ
Is injection molding always required for medical plastic parts?
No. Below a few thousand units per year, or while the design is still changing, CNC machining is usually cheaper and faster. Mold only when volume and design are stable.
Which plastic survives autoclave sterilization?
PP, PE, PEI (Ultem), PEEK, PPSU, and LSR tolerate autoclave steam well. Many PC grades risk hydrolysis or yellowing and are better paired with gamma or EtO. Confirm against the specific grade’s data.
What does ISO 13485 mean for my molded part?
It means the molder runs a documented quality system with validation (IQ/OQ/PQ) and lot-level traceability — the manufacturing evidence your device submission needs.
Can a metal part be overmolded?
No. A metal or ceramic core must be encapsulated by insert molding. Overmolding bonds a second material onto an already-molded plastic substrate.
How do I choose a medical molding supplier?
Check ISO 13485 scope, engineering/DFM support, material certification, traceability, and IP handling — then compare price. Use a supplier audit checklist.