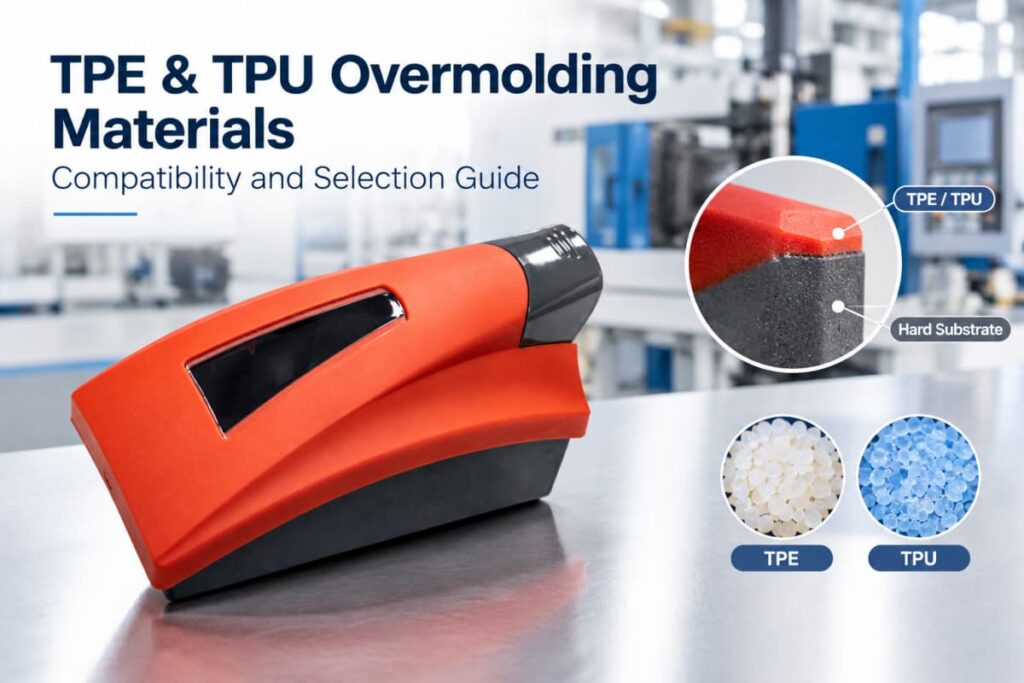
The short answer to material selection for overmolding materials is this: a soft layer bonds to a rigid substrate only when the two resins are chemically compatible or when the geometry forces a mechanical interlock. Pick a TPE or TPU whose polarity and melt temperature match the substrate, and the bond holds under load and thermal cycling. Pick the wrong pair and the overmold peels off like a skin. This guide explains how to choose the substrate–elastomer combination, what breaks the bond, and how suppliers verify adhesion before production.
What Determines Overmolding Bond Strength
Overmolding relies on two bonding mechanisms, and a reliable part usually uses both.
Chemical adhesion forms when the molten elastomer shares polarity or a base resin with the substrate and is hot enough to partially re-melt the substrate surface. The two materials inter-diffuse at the interface and cross-link as they cool. Chemical bonds are strongest when the substrate and overmold come from the same resin family—for example, a polypropylene-based TPE (TPE-S / SEBS on PP) over a PP substrate.
Mechanical interlocking is the fallback when chemistry is weak. The designer adds holes, undercuts, grooves, or a textured surface to the substrate so the flowing elastomer fills those features and locks in place as it solidifies. This is the standard approach for non-polar substrates such as PP bonded to a dissimilar TPE, or for any pair where a chemical bond cannot be guaranteed.
In practice, the bond rarely fails for one reason alone. Contamination on the substrate surface, a second shot that is too cold, or moisture in a hygroscopic resin each reduce interfacial strength. Good designs combine a compatible resin pair with enough geometric interlock to survive handling, shipping, and end-use stress.
Common Substrate and Overmold Pairs
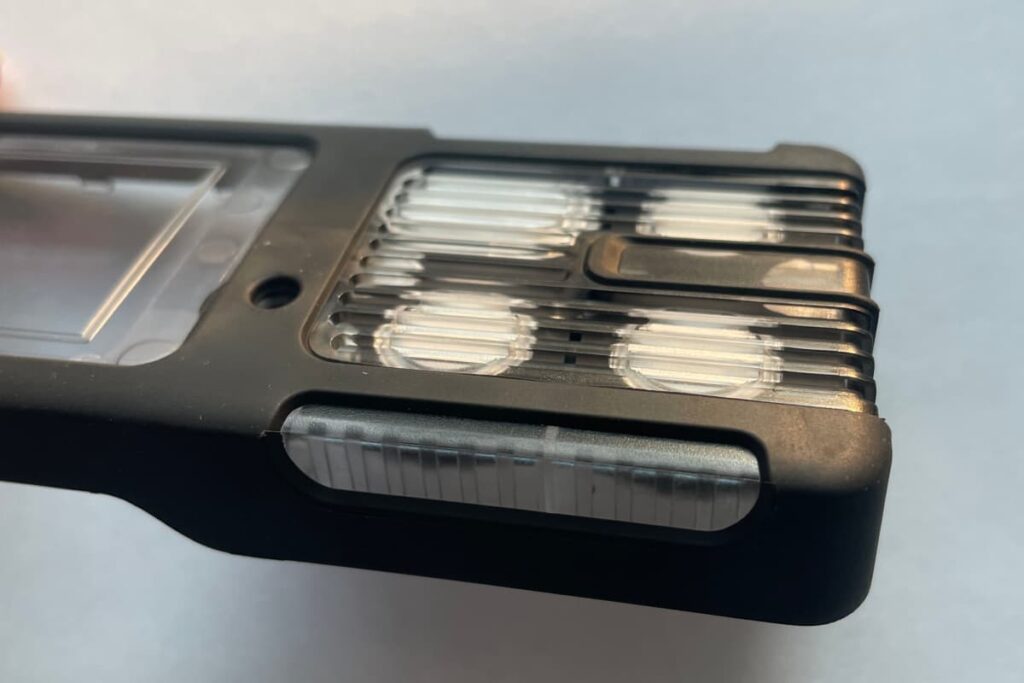
The table below lists substrate–elastomer combinations that are routinely used in production. Treat it as a starting point: adhesion varies by grade, filler, mold surface, and process window, so confirm any pair with a bond test before committing to tooling.
| Substrate | Compatible Overmold | Bonding Mechanism | Typical Use |
|---|---|---|---|
| ABS | TPU, TPE-S (SEBS) | Chemical | Power-tool grips, enclosures |
| PC | TPU, TPE-S | Chemical | Electronic housings, lenses surrounds |
| PP | TPE-S (PP-based SEBS) | Chemical | Containers, hinges, seals |
| PC/ABS | TPE-S, TPU | Chemical | Laptop and device shells |
| PA6 / PA66 (Nylon) | TPO, TPU | Mechanical + Chemical | Automotive connectors, clips |
| SAN | TPU | Chemical | Consumer handles |
| POM (Acetal) | Limited — mechanical only | Mechanical | Low-cost goods (verify) |
| Any rigid plastic | Incompatible soft elastomer | Mechanical (undercuts) | Cost-sensitive parts |
A few rules of thumb apply across most programs. For polyolefin substrates (PP, PE), use a polyolefin-based TPE; for engineering resins (ABS, PC, PA), use a styrenic or TPU-based elastomer. When suppliers claim a TPE “bonds to everything,” it usually bonds well to two or three substrates and poorly to the rest—always request a sample before tooling.
For a broader view of substrate options and how each resin behaves in molding, see our engineering plastics selection guide.
TPE vs TPU: Choosing the Overmold Elastomer
TPE (thermoplastic elastomer, often SEBS- or TPO-based) and TPU (thermoplastic polyurethane) are the two elastomers most often specified for overmolding. They are not interchangeable.
TPE (SEBS / TPO) is softer, cheaper, and easier to process. It is the default for soft-touch grips, seals, and consumer goods where durometer in the 30A–80A range is enough. SEBS bonds chemically to polar and polyolefin substrates when the base resin matches. It has lower oil and abrasion resistance than TPU.
TPU is tougher, more abrasion-resistant, and resists oils and many chemicals. It holds detail better and survives harsher environments, which is why it appears in automotive, industrial, and cable-protective overmolds. TPU bonds well to ABS and PC and can bond to nylon with the right grade and surface preparation, but it is hygroscopic and must be dried before molding.
Choose TPE when the priority is a comfortable, low-cost soft surface. Choose TPU when the part sees abrasion, oil, or mechanical load. Both can be colored and textured, so aesthetics alone do not decide the choice.
What Weakens or Breaks the Bond
Bond failure in overmolding shows up as peeling, lifting at edges, or delamination after thermal cycling. The usual causes are preventable:
- Surface contamination — mold release, oil, or dust on the substrate blocks chemical adhesion. Keep the substrate clean and avoid excess release agent.
- Second shot too cool — if the elastomer does not re-melt the substrate surface, no inter-diffusion occurs. Process windows must keep the interface hot enough at the moment of the second shot.
- Moisture in hygroscopic resins — nylon and TPU absorb water; unmelted moisture causes splay and a weak interface. Dry the material to spec before molding.
- Mismatched shrinkage — the substrate and overmold shrink at different rates. If the mold is cut to nominal dimensions without shrink compensation for both layers, the part can warp or the bond line can open.
- Insufficient interlock on non-polar pairs — PP bonded to a dissimilar TPE needs undercuts or texture; a flat interface will not hold.
These failure modes are closely related to general molding defects, and many are caught during first-article validation. Our defect prevention guide covers overlapping causes.
How Bond Strength Is Verified Before Production
A material pair should be proven before volume tooling is cut. The typical verification path is:
- Bond test sample — mold or prototype a small coupon of the exact substrate–elastomer pair.
- Peel or pull test — measure adhesion in Newtons; the number matters less than consistency and whether the failure is cohesive (within the elastomer, good) versus adhesive (at the interface, bad).
- Environmental cycling — expose samples to heat–cold, humidity, and any chemical the part will see, then re-test.
- Microsection — cut and inspect the interface to confirm inter-diffusion or mechanical lock.
- T1 validation — once tooling exists, the first molding (T1) confirms the bond on the real part, not just a coupon.
Our T1 sample evaluation guide explains how first-article parts are checked before a program moves to production.
Material Selection Decision Framework
Use this sequence when specifying an overmolded part:
- Step 1 — Fix the substrate. It is usually set by structural, chemical, or regulatory needs (e.g., PC for clarity, PP for chemical resistance, nylon for strength).
- Step 2 — Match the elastomer family. Polyolefin substrate → polyolefin-based TPE; engineering substrate → styrenic or TPU.
- Step 3 — Set the hardness and environment. Soft grip at room temperature → TPE; abrasion, oil, or load → TPU.
- Step 4 — Decide the bond path. Strong chemical match → rely on adhesion; weak or risky match → add undercuts, grooves, or texture for mechanical interlock.
- Step 5 — Require a bond test. Do not skip this for any production program.
The same part still has to be manufacturable, so the material choice feeds directly into the design rules covered in our overmolding design guidelines.
Matching Materials to Application
Different industries weight the bond differently:
- Medical — chemical-resistant, bondable grades with documentation; soft grips on instruments and sealed housings. See our medical injection molding trends for context.
- Automotive — TPU for abrasion and under-hood or exterior exposure; nylon substrates with mechanical interlock for connectors.
- Consumer electronics — PC/ABS with TPE-S for housings and seals; tight bond lines matter for appearance. Our consumer electronics molding guide covers related requirements.
- Power tools and hardware — PP or nylon substrates with TPE/TPU grips for ergonomics and vibration damping.
When the part could also be made by a different multi-material process, compare the trade-offs in our two-shot molding vs overmolding and insert molding vs overmolding guides.
Key Takeaways
- Overmolding bonds form through chemical adhesion, mechanical interlocking, or both—design for the mechanism your material pair actually supports.
- Match the elastomer family to the substrate: polyolefin-based TPE for PP/PE, styrenic or TPU for ABS/PC/PA.
- Choose TPE for low-cost soft touch; choose TPU for abrasion, oil, and load.
- Contamination, a cold second shot, moisture, and uncompensated shrinkage are the main causes of bond failure.
- Always validate the pair with a bond test and T1 sample before cutting production tooling.
FAQ
Can any TPE bond to any plastic?
No. Adhesion depends on polarity and melt-temperature match. A TPE that bonds well to ABS may not bond to PP without mechanical interlock. Confirm with a bond test.
Is TPU better than TPE for overmolding?
Neither is universally better. TPU resists abrasion, oil, and load; TPE is softer and cheaper. The right choice follows the end-use environment.
How thick should the overmold layer be?
Typical overmold layers run about 1.5–3 mm. Below roughly 1 mm you risk short shots; above about 4 mm you risk sink marks and long cooling. Exact values depend on the resin and part.
Do I need a bond test if the supplier says the materials are compatible?
Yes. Grade, filler, surface finish, and process window change the result. A sample bond test is the only way to confirm the pair for your specific part.
Tell us your substrate, target hardness, and the environment the part will see—chemical, thermal, or mechanical. We will recommend a TPE or TPU grade and run a bond test sample so you can validate adhesion before tooling. Start from our Overmolding & Multi-Shot Injection Molding Services page or contact our engineering team.